
Every motor, compressor, speaker and car door makes noise, and that noise tells engineers a lot about product quality. But you can only measure it properly when the room around the product stays silent. That is why R&D labs, automotive units and electronics makers invest in purpose-built test rooms. Picking the right Soundproof Chamber Manufacturer decides whether your readings can actually be trusted.
What Is a Soundproof Chamber?
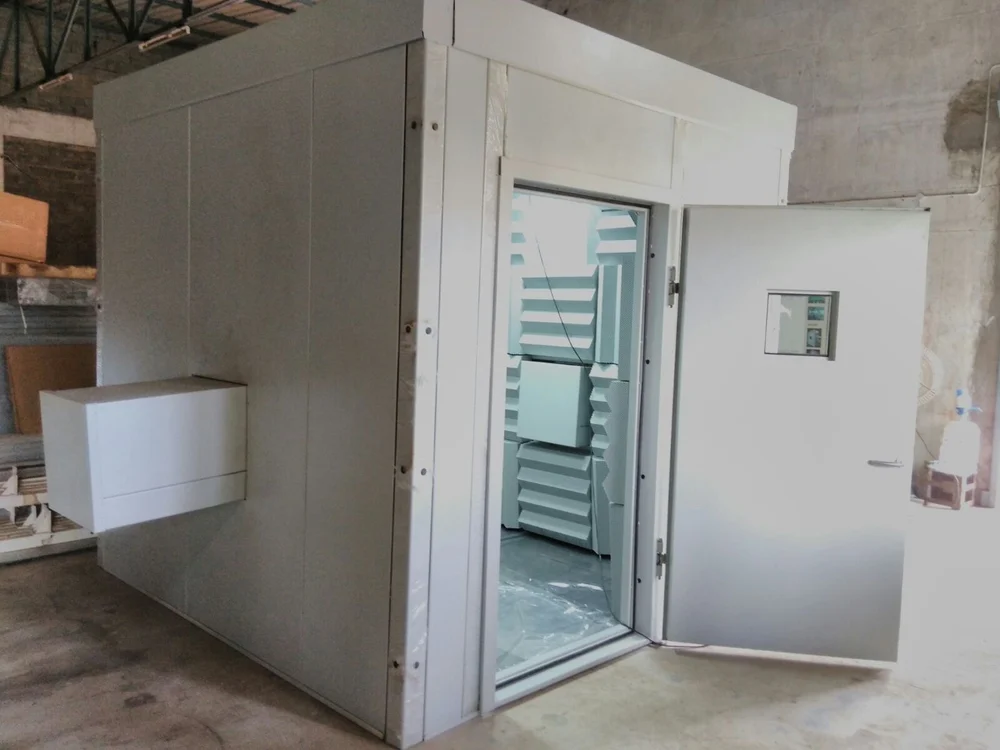
A soundproof chamber is an engineered room that blocks outside noise and controls the sound inside it. Layered steel, mineral wool and absorptive lining keep traffic, machinery and voices away from the microphone.
Types of Chambers and Where They Fit
Different tests call for different rooms.
- Anechoic chamber: absorbs almost every reflection, so sound behaves as it would in open space. Ideal for product development and sound power measurement.
- Reverberation chamber: does the opposite, using hard surfaces to create an even sound field. Used for absorption and transmission loss tests.
- NVH test chamber: a quiet room for evaluating noise, vibration and harshness in vehicles, appliances and components.
- Noise test booth: a compact enclosure for quick checks on smaller parts near the production line.
Key Factors to Check Before You Decide
Acoustic performance. Ask for the background noise level and the lowest frequency the chamber can handle. A good Soundproof Chamber Manufacturer will give you numbers, not vague promises.
Structural design. Floating floors, vibration isolation and door seals matter as much as the wall panels.
Ventilation and services. Test rooms still need fresh air, lighting and cable access. Silencers and acoustic louvers let air move without letting noise leak in.
Customisation. Your sample size, test standard and floor space are unique. Modular construction lets the room fit your site and grow later.
Experience and certification. Look for ISO-certified processes, a record of completed projects and in-house manufacturing. These keep quality consistent and delays low.
Common Mistakes Buyers Make
Choosing on price alone is the biggest one. A cheaper room that cannot reach the required noise floor gives unusable data, and rebuilding it costs far more than doing it right the first time. Another mistake is ignoring the site. Nearby traffic, building vibration and ceiling height all shape the design, so share these details early. An experienced Soundproof Chamber Manufacturer will ask about them before quoting.
A Closer Look at a Trusted Manufacturer
SomNandi Industries designs and builds anechoic chambers, NVH test chambers, reverberation chambers and noise test booths from its 80,000 sq ft manufacturing facility in Greater Noida. Its engineers tailor every room to the test standard and the space available. As a Soundproof Chamber Manufacturer working across design, fabrication and installation, the team keeps the whole process under one roof.
Planning Your Project Step by Step
Start with the tests you plan to run, the frequency range and the size of your samples. Then share floor plans and site conditions with two or three shortlisted suppliers and compare their proposals line by line. Ask about installation time, after-sales support and help with calibration.
Final Thoughts
A test chamber is a long-term asset, not a one-time purchase. The right Soundproof Chamber Manufacturer will listen to your requirements, explain the trade-offs honestly and deliver a room that performs year after year. Whether you are building a new lab or upgrading an old one, SomNandi Industries can help you turn a noisy problem into a controlled, measurable environment where every test result counts.
- How-to-Choose-the-Right-Soundproof-Chamber-Manufacturer-for-Accurate-Acoustic-Testing
How-to-Choose-the-Right-Soundproof-Chamber-Manufacturer-for-Accurate-Acoustic-Testing